China Top 10 Superior Quality Machine Suppliers?
Choosing a superior quality machine supplier in China takes more than comparing prices or polished product photos. Buyers need to examine the machine’s working range, component quality, inspection records, and support after delivery. A supplier’s factory tour can reveal practical details: organized assembly stations, calibrated measuring tools, and technicians testing equipment under load. Small signs matter.
Quality expert Joseph M. Juran described quality as “fitness for use.” That principle suits industrial purchasing: a machine must perform reliably in the buyer’s actual production setting, not merely look impressive in a catalogue. This guide introduces ten Chinese machine suppliers and outlines what buyers should verify before requesting a quotation. The list should be treated as a starting point, not a universal ranking; capabilities vary by model, application, and order requirements.
The comparison considers product specialization, manufacturing experience, quality-management practices, customization, documentation, and technical service. Buyers should also confirm relevant certificates directly, review sample inspection reports, and ask how spare parts are supplied. A video call may help, but it cannot replace a clear contract and a properly defined acceptance test. Details can be missed. Even a capable supplier may not suit every factory. Use the profiles to narrow the field, then check specifications against your materials, output targets, installation conditions, and maintenance resources. A careful shortlist takes time, but it can prevent costly mismatches later.
Define China’s Machine-Supplier Scope Across CNC, Forming, and Industrial Systems
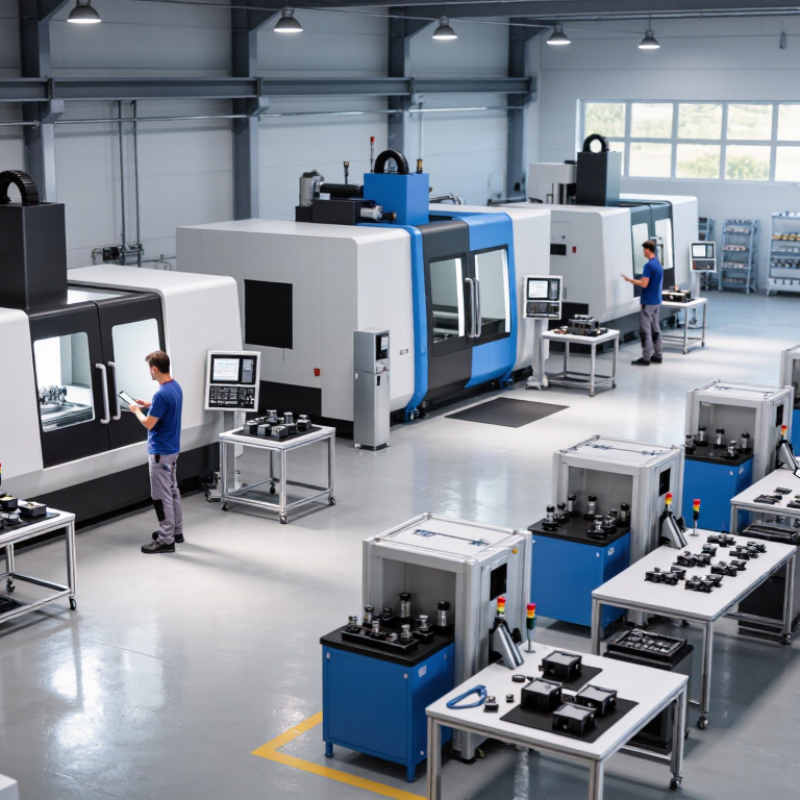
A useful comparison of China’s machine suppliers starts with a clear scope. CNC suppliers make equipment such as turning centers, milling machines, and machining centers. Forming suppliers focus on presses, bending equipment, and metal-shaping systems. Industrial-system suppliers may integrate automation, material handling, and production-line controls.
These categories overlap. A CNC machine may arrive with robotic loading, while a forming line can include inspection and safety systems. The boundary matters. Buyers should compare the machine itself and the supporting engineering separately. Check workpiece dimensions, spindle or pressing capacity, control functions, and installation requirements. Ask for evidence. Request test records, component specifications, service procedures, and references for similar applications. A polished brochure cannot confirm how a machine performs on a real factory floor.
Supplier evaluation also depends on the buyer’s production conditions. Ask how the machine handles the actual material, tolerance, cycle time, and shift pattern. Review commissioning plans, operator training, spare-parts availability, and response arrangements. These details can reveal gaps before shipment. Still, supplier categories are not perfectly neat; an integrated system may be difficult to compare with a standalone machine. That is a real limitation, not a reason to ignore the distinction. Define the scope before requesting quotations, then compare like with like.
Set Top-10 Selection Criteria Using ISO 9001:2015 Quality-System Requirements
Selecting ten superior machine suppliers should begin with evidence, not showroom polish. ISO 9001:2015 offers a useful baseline: clauses 4–10 cover organizational context, leadership, planning, support, operations, performance evaluation, and improvement. Certification alone cannot prove a machine will hold tolerance on your shop floor. Certificates can mislead.
ISO’s 2022 Survey of Management System Standard Certifications recorded 1,265,216 ISO 9001 certificates across 189 countries. Verify each supplier’s certificate validity, scope, manufacturing site, and certification body’s accreditation status. Then assess practical controls: design reviews, approved sub-suppliers, material traceability, calibrated gauges, final inspection records, and corrective actions. Ask for a recent nonconformance case and evidence that its root cause was addressed.
Use measurable performance, not promises. Compare first-pass acceptance, on-time delivery, warranty claims, and response times over a defined period. During a factory visit, match a gauge’s calibration label to its register, then trace one component from incoming inspection to final testing. Small details matter. Some suppliers maintain excellent records but struggle when specifications change; test their change-control process with a real revision. ISO 9001:2015 clauses 9.1 and 10.2 support performance monitoring and corrective action. Rank candidates after technical trials and reference checks.
China Top 10 Machine Supplier Selection Criteria
Suggested evaluation weights aligned with ISO 9001:2015 requirements
Use these suggested weights to compare machine suppliers when identifying a shortlist of ten. ISO 9001:2015 sets quality-management-system requirements; it does not rank suppliers or prescribe evaluation weights. Verify each supplier’s evidence, including certification scope and relevant operational records.
Verify Machine Accuracy with ISO 230-2:2014 Positioning Tests
When comparing machine suppliers, ask for axis-level evidence, not a headline accuracy figure. ISO 230-2:2014 specifies tests for positioning accuracy and repeatability of numerically controlled axes, including measurements from both directions. Request the test positions, travel length, ambient temperature, warm-up state, and raw readings. A laser interferometer can reveal reversal error when an axis approaches the same point from opposite directions. Small detail. Big consequence.
A useful report separates machine error from measurement uncertainty. NIST Technical Note 1297 explains expanded uncertainty; for a normal distribution, a coverage factor of k=2 corresponds to about 95% coverage. Ask suppliers to state the uncertainty and coverage factor beside each result, not hide them in a footnote. Compare results with the tolerance for your process, such as a bore pattern, rather than a brochure figure. ISO testing supports a fair comparison, but it cannot guarantee production accuracy under every load or temperature. I would repeat critical tests after thermal stabilization, too. A precise-looking number can still mislead.
China Top 10 Superior Quality Machine Suppliers? — Verify Machine Accuracy with ISO 230-2:2014 Positioning Tests
Ten evidence points for comparing machine suppliers without presenting unverified supplier rankings or performance claims.
| No. |
Comparison dimension |
What to verify |
Evidence to request |
Assessment status |
| 1 |
Applicable standard |
Confirm the positioning test was conducted with reference to ISO 230-2:2014 for numerically controlled machine-tool axes. |
Test report naming the standard, edition, machine model, serial number, and axis tested. |
Verify report |
| 2 |
Axis and travel tested |
Check which linear or rotary axis was tested and whether the measured travel represents the usable working range. |
Axis identification, test travel, measurement positions, and machine configuration. |
Verify report |
| 3 |
Measurement positions |
Confirm that the test positions and approach sequence are documented and appropriate to the axis travel and test plan. |
Position list or plot showing commanded and measured positions. |
Verify report |
| 4 |
Approach directions |
Check that measurements distinguish positioning from both approach directions where bidirectional results are reported. |
Separate results for positive and negative approach directions, where applicable. |
Verify report |
| 5 |
Positioning accuracy |
Review the reported unidirectional and bidirectional positioning accuracy values for each tested axis. |
Numerical results and the report’s stated calculation method and units. |
Compare with requirement |
| 6 |
Positioning repeatability |
Review repeatability results by approach direction and the bidirectional repeatability result, when reported. |
Repeated measurement data and calculated repeatability values. |
Compare with requirement |
| 7 |
Reversal error |
Check the reported difference associated with approaching the same position from opposite directions. |
Reversal-related results by position or axis, with units and calculation details. |
Review results |
| 8 |
Measurement system |
Confirm the measuring instrument is suitable for the test and that its calibration is current and traceable. |
Instrument type, resolution, calibration certificate, and calibration validity dates. |
Verify records |
| 9 |
Test conditions |
Review the documented machine state and environmental conditions, including relevant thermal conditions. |
Pre-test procedure, warm-up details, ambient conditions, and any deviations from the test plan. |
Review records |
| 10 |
Acceptance criteria and traceability |
Compare measured results with the buyer’s stated accuracy requirement; ISO test results alone do not establish suitability for every application. |
Signed report linked to the delivered machine’s model and serial number, plus agreed acceptance limits. |
Buyer decision |
Note: This is a supplier-evaluation checklist, not a ranked list of companies or a record of actual supplier test results. Request machine-specific, traceable ISO 230-2:2014 test reports before making a purchasing decision.
Compare Productivity Using OEE: Availability × Performance × Quality
When comparing China’s top machine suppliers, quoted speed tells only part of the story. OEE offers a more practical view: Availability × Performance × Quality. A machine may run quickly during a demonstration, yet lose hours to changeovers, minor jams, or maintenance delays. Ask suppliers for shift-level production records, not just brochure figures. Check whether downtime categories and inspection methods are clearly defined.
Consider a line with 90% availability, 95% performance, and 98% quality. Its OEE is about 83.8%, not 95%. That difference matters. Review actual cycle times, rejected-part counts, and recovery time after stoppages. A simple log beside the machine can reveal patterns that a polished dashboard misses. Small details count.
Still, OEE is not a complete verdict. Product mix, operator training, and planned maintenance can change the result. Supplier trials should use representative materials and realistic shift conditions. I would also question unusually perfect data; some losses may be recorded inconsistently. That is easy to overlook. A transparent supplier should explain the calculation, share raw observations, and discuss what the figures leave out.
Profile Suppliers by Product Range, Export Records, and Service Coverage
A useful review of China’s top machine suppliers should compare more than polished catalogs. Start with product range: check whether each supplier builds one machine type or supports a complete production line. Look for model specifications, materials, output rates, and optional configurations. Ask for drawings or a sample quotation tied to your application. A broad catalog is not proof of deep manufacturing capability.
Export records offer another practical signal. Request examples of recent shipments, destination markets, and references from buyers using comparable equipment. Verify what can be checked, such as packing lists, inspection reports, and commissioning records. Paperwork matters. A supplier may have export experience but little experience with your machine category, so treat general claims carefully.
Service coverage can determine whether a machine remains productive after delivery. Compare response times, installation support, spare-parts availability, manuals, and remote troubleshooting. Ask who handles service and what happens when a technician cannot visit promptly. These details are easy to overlook during price negotiations. Not everything travels well. A low quotation may exclude training or essential parts, while a strong service promise may lack clear terms. Record the answers in a comparison sheet, and note unanswered questions rather than filling gaps with assumptions. That makes a ten-supplier shortlist more useful, though the scoring still needs human judgment.